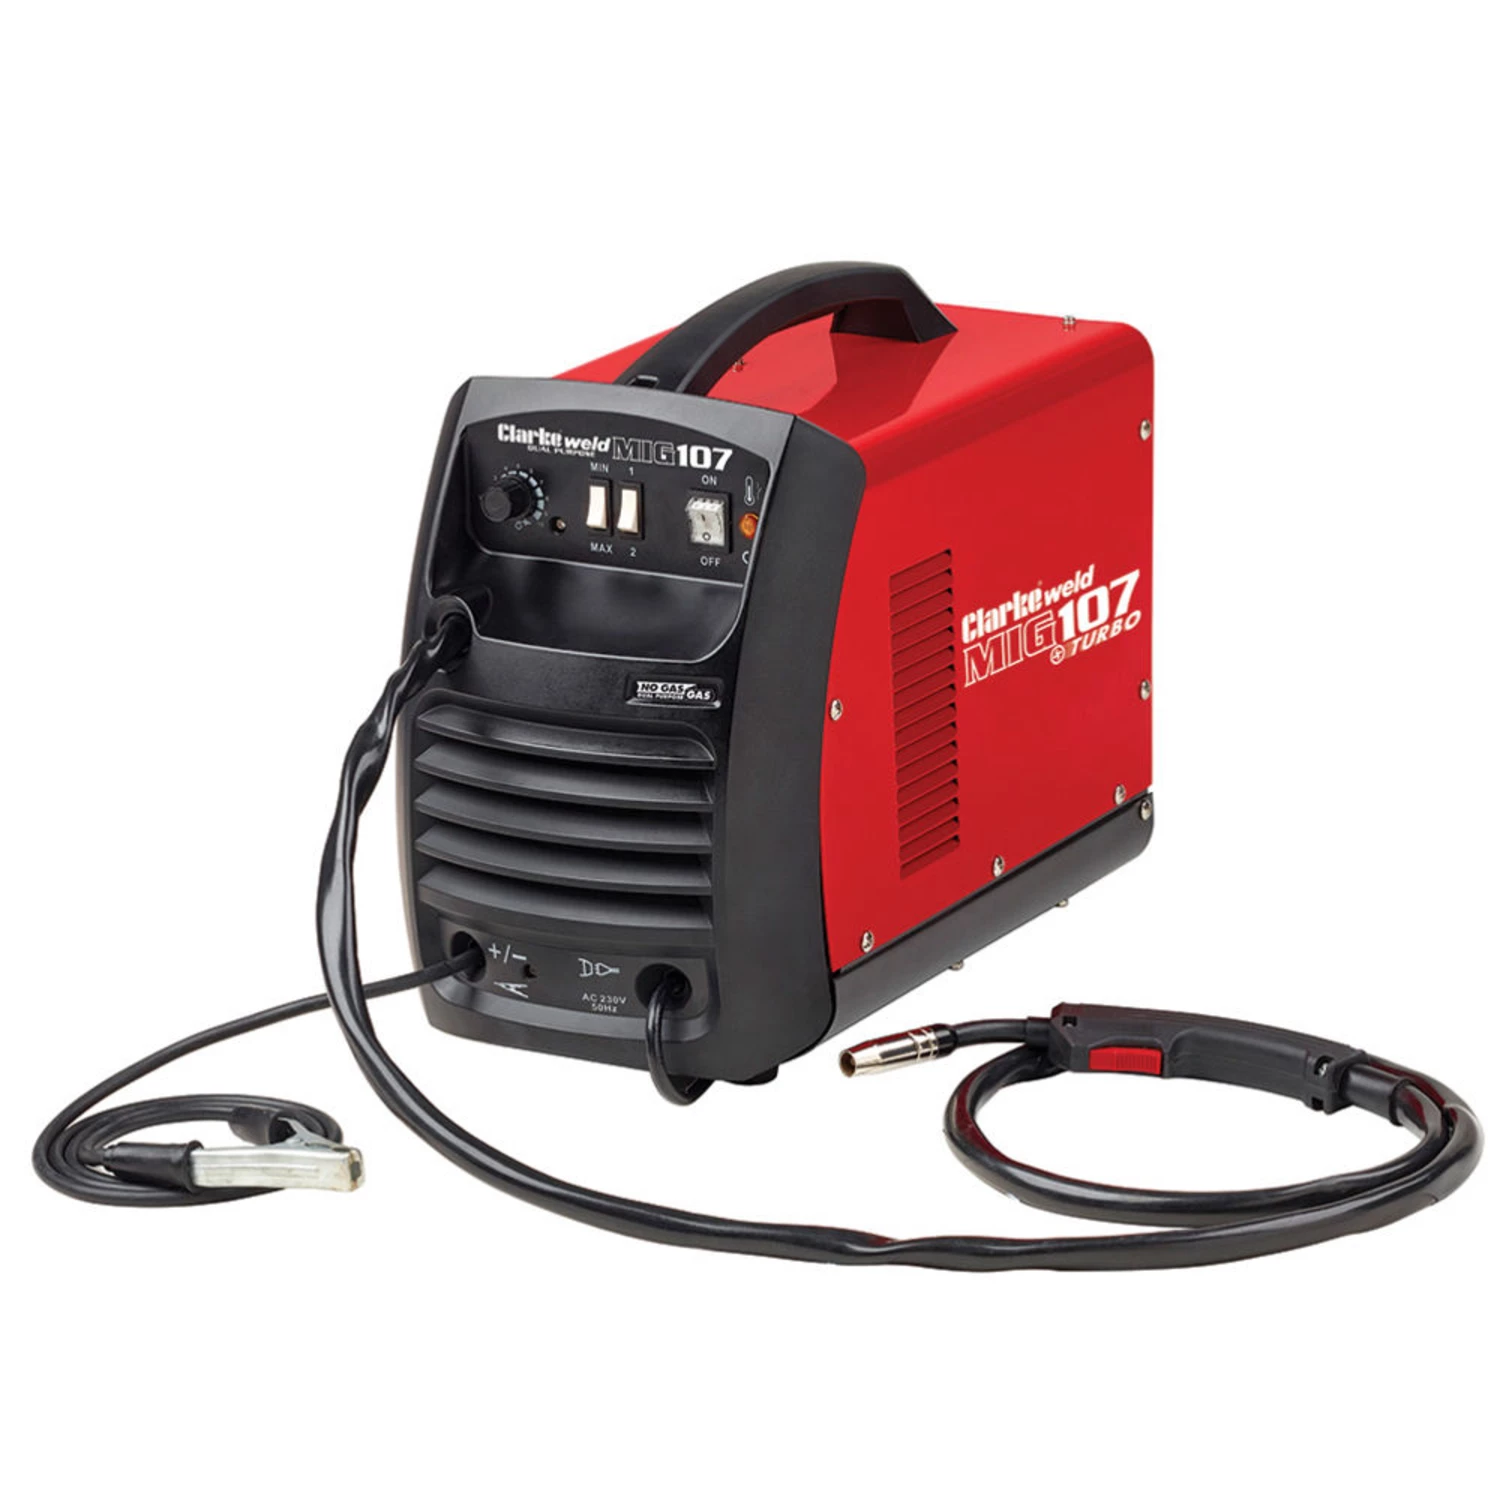
Pick A
Clarke MIG107 No Gas/Gas 100Amp (230V)
Entry MIG path researched for gas / no-gas flexibility on UK 230V — relevant to this gas vs flux-cored topic. Untested.
Untested View on Machine MartWhen cylinder-gas MIG fits — and when self-shielding flux-cored (no-gas) is the practical outdoor choice — before you buy wire or a machine.
Affiliate disclosure: This page contains affiliate links. We may earn a commission if you buy through them. Nothing here is a paid ranking. Gear cards below are research / Untested — not personal on-site reviews. Process advice is general, not a welding procedure specification.
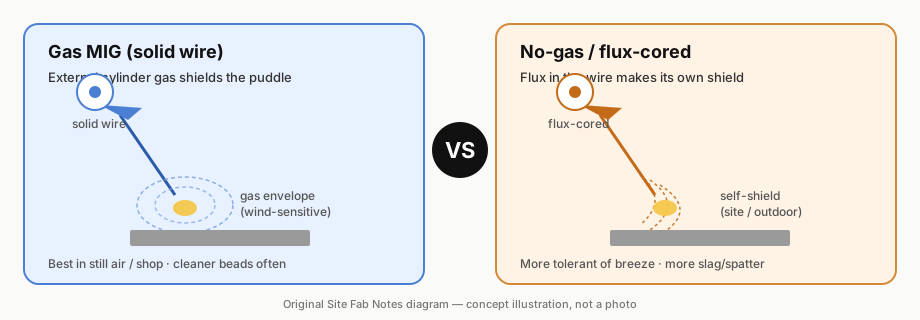
Solid wire plus an external shielding gas (often Argon/CO2 mix for mild steel). The gas envelope keeps air off the puddle. Wind can strip that shield — porosity risk rises outdoors without screens or calm conditions.
Self-shielding flux-cored wire carries flux that generates its own shield as it burns. Often discussed for outdoor site work where cylinders and wind are awkward. Expect slag to chip and typically more spatter clean-up.
UK site note: Match wire type, polarity, and tip to the datasheet for your machine. This page does not certify any unit for outdoor use or claim we have run these products on site.
| Factor | Gas MIG | No-gas / flux-cored |
|---|---|---|
| Wind / outdoor | Sensitive — screen or wait for calm | More tolerant (self-shield) |
| Clean-up | Often less slag; spatter varies | Slag + often more spatter |
| Logistics | Cylinder + regulator + hose | Wire spool; no cylinder for self-shield |
| Shop / still air | Common everyday choice | Works; clean-up trade-off |
| Consumables | Solid wire + gas volume | Flux-cored wire (cost per kg differs) |
| Typical UK use | Yard / garage / screened fab | Site frames, outdoor repairs |
Research placement only. No on-site use claims. Links go to Machine Mart via Awin.
Entry MIG path researched for gas / no-gas flexibility on UK 230V — relevant to this gas vs flux-cored topic. Untested.
Untested View on Machine Mart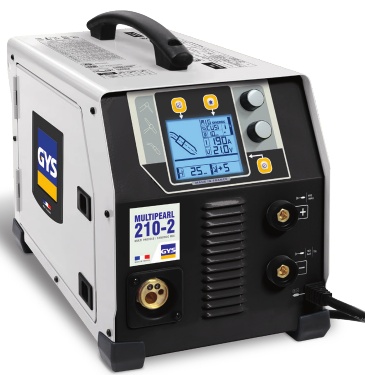
Higher-amp multi-process research option when MIG plus occasional other processes matter more than a small gas/no-gas starter.
Untested View on Machine Mart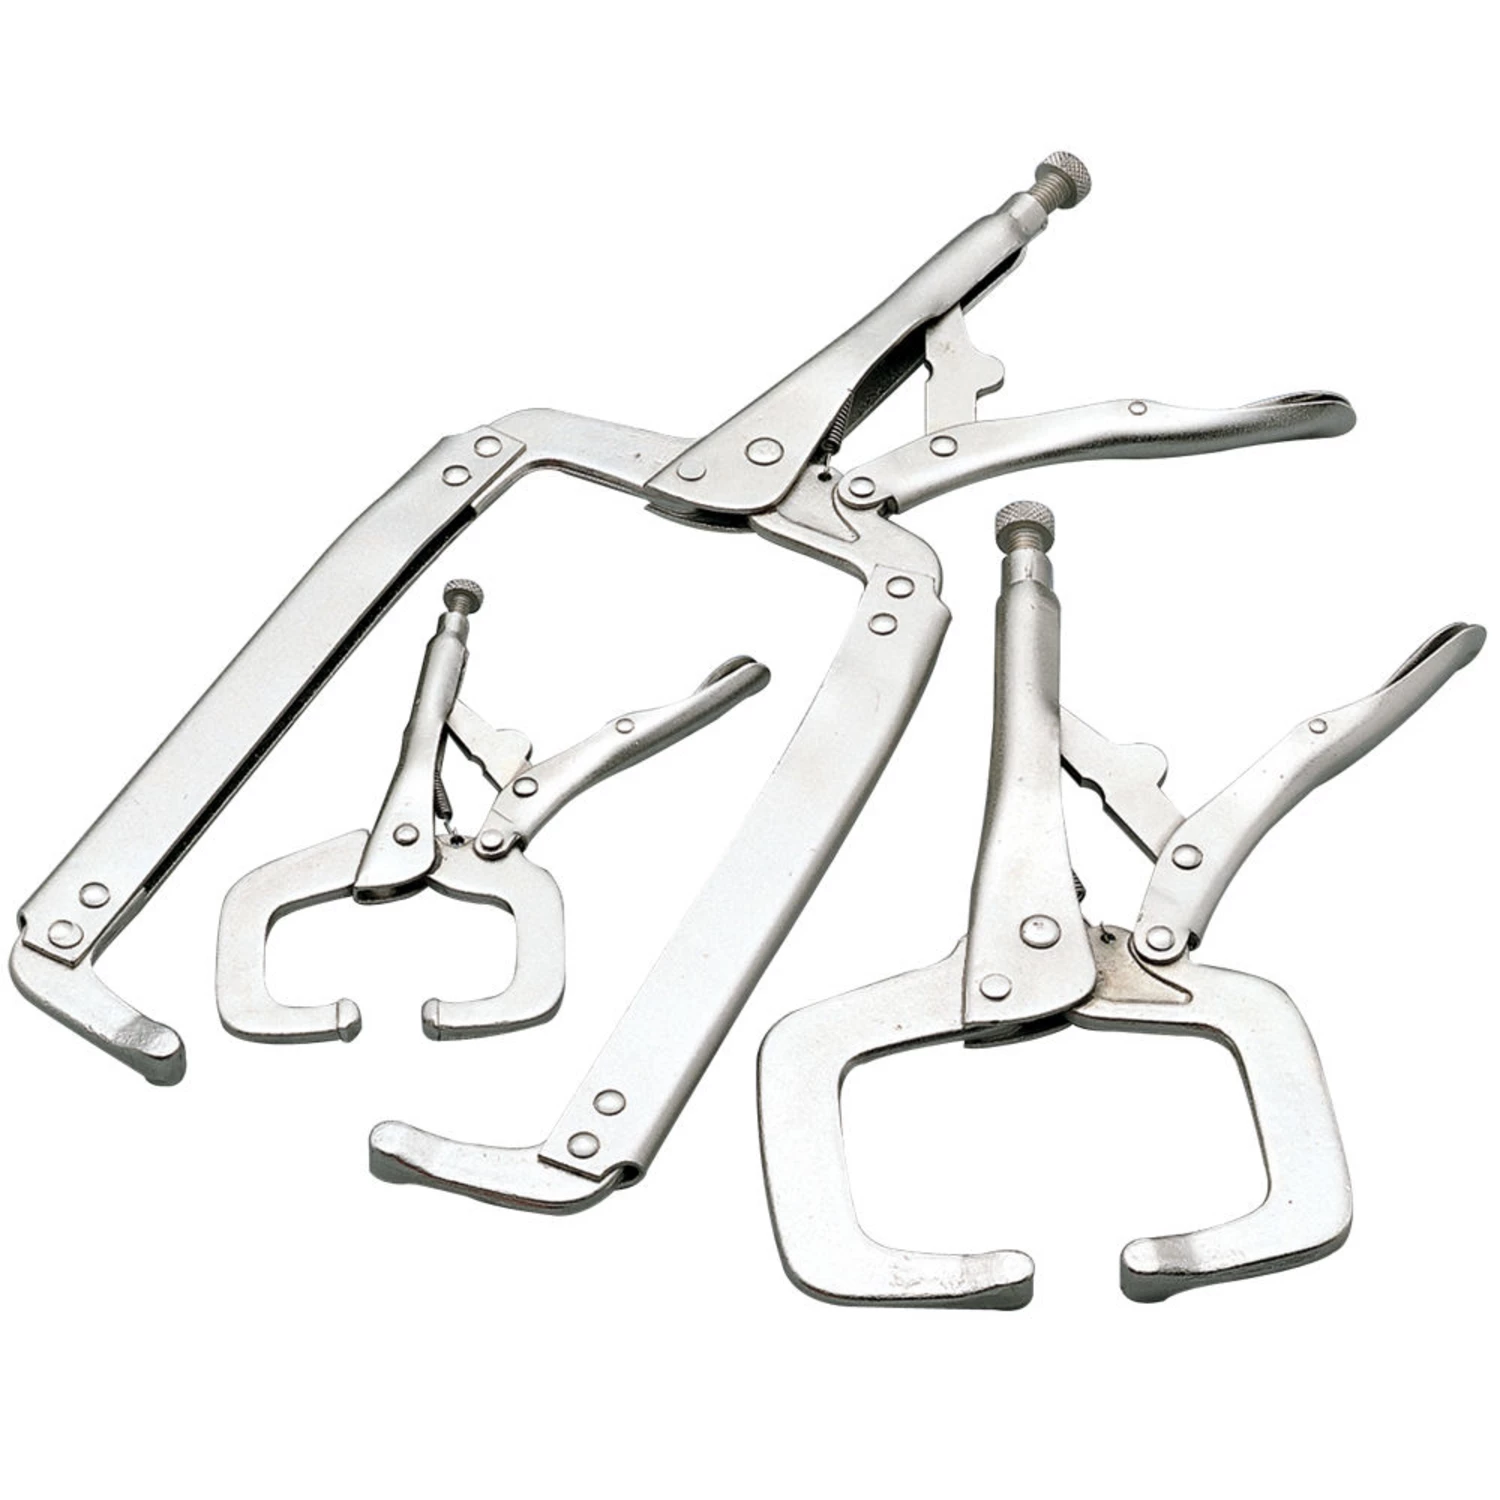
Fit-up aid for tacking outdoor assemblies. Complements process choice — not a welder.
Untested View on Machine MartGas MIG (solid wire with cylinder gas) works best when wind is low or you can screen the joint — still air, sheltered yards, and indoor fab. A breeze can blow the shield away and leave porosity. It is not a WPS; follow your job and employer rules.
Self-shielding flux-cored (no-gas) wire is often discussed for breezy outdoor and site work because the flux generates its own shield. Expect more slag and spatter clean-up than gas MIG in still air. Match wire polarity and machine settings to the wire datasheet.
Some entry MIG units advertise gas and no-gas / flux-cored modes. That flexibility can suit mixed shop and outdoor work, but changeover needs the right wire, tips, and polarity. Treat retailer claims as research, not a guarantee for your machine.
No. If you can control wind (screens, indoor bay, calm day), gas MIG often gives cleaner beads with less slag. Flux-cored earns its keep when wind or logistics make cylinders awkward — trade-offs, not a universal rule.
No. This is general research for UK domestic and site mild-steel fab. Coded or contract work follows your written WPS, employer procedures, and applicable standards — not this page.
No. Product cards are labelled Untested research placements with Machine Mart affiliate links. We do not claim on-site use of the named machines.